


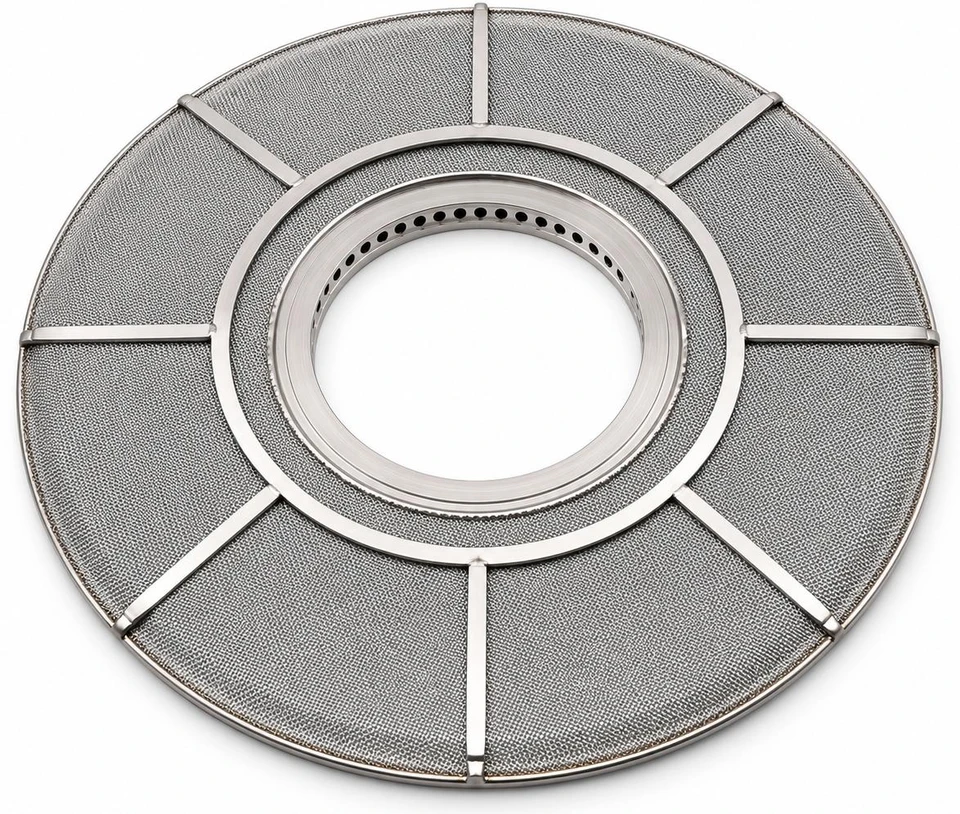
Leaf disc filters provide compact filtration area for polymer melt processing. Selecting the medium and complete disc assembly together helps control contamination before the melt reaches the film die.
Leaf Disc Filters
For Polymer Melt and Film Filtration
Filtration Before Film Formation
BOPET
Biaxially Oriented Polyethylene Terephthalate.
A polyester (PET) film used in packaging, electrical insulation and industrial applications.
BOPA
Biaxially Oriented Polyamide.
A polyamide (PA) film, commonly called nylon film, used in packaging.
BOPP
Biaxially Oriented Polypropylene.
A polypropylene (PP) film used in flexible packaging and labels.
Biaxially oriented means the film is stretched in two directions: along its length and across its width.
Engineered for the Process
These filters target gels, catalyst residues and other solid contaminants in film production. Match the filter to the polymer, throughput, equipment drawing and required film quality.
Construction and Operating Principle
How Melt Passes Through the Disc
The pressure difference between the unfiltered melt in the housing and the filtered melt in the central collector drives flow through both faces of each disc. The diagram shows one radial half section, from the sealed outer edge to the central hub.
How a Leaf Disc Filter Works
Two Filtering Faces | Radial Drainage | Central Collection
Radial Flow Through a Leaf Disc
Filtered melt flows inward through the drainage core to the central collector. Conceptual section; construction varies by design.
1Filter Medium
Retains contaminants as melt passes through the two filtering faces.
2Unfiltered Polymer Melt
Melt in the housing before it passes through the filter medium.
3Hub / Seal
Connects the disc to the collector and seals the interface against bypass.
4Central Collector
Receives filtered melt from the disc stack and carries it to the system outlet.
5Hub Outlet
Provides the passage from the internal drainage core into the collector.
6Filtered Melt
Melt leaving the disc after passing through the filter medium.
7Support Layers
Support the filtering faces while allowing melt to pass into the drainage core.
8Sealed Outer Edge
Closes the outer perimeter to prevent melt bypassing the filtering faces.
9Internal Drainage Core
Carries filtered melt radially inward towards the hub.
Filtration Sequence
Melt Entry
Unfiltered polymer fills the spaces between adjacent discs and contacts the upper and lower filtering faces.
Filtration
Melt passes through the porous medium on each face.
The selected medium retains contaminants; the supporting layers maintain the filtering structure.
Radial Drainage
After passing through the medium, the filtered melt enters the internal drainage core and travels radially inward towards the hub.
Central Collection
Melt passes through the hub outlets into the common collector, which carries the combined flow from the disc stack to the system outlet.
Why Sealing and Spacing Matter
The sealed outer edge and hub interface prevent melt from bypassing the medium. Correct inter disc spacing maintains access to both faces and supports consistent flow distribution.
Technical Specifications
Published Range and Rating Basis
Confirm applicability to the selected medium, disc construction and assembled stack before ordering.
Filtration Grades
5, 7, 10, 15, 20, 25, 30, 40, 60, 80 and 100 µm at βx ≥ 75
What βx ≥ 75 Means
The beta ratio compares upstream and downstream particle counts at or above size x. A ratio of 75 corresponds to approximately 99% removal under the applicable particle count test conditions.
Request the test method, fluid, challenge particles and operating conditions for the quoted grade. Confirm the applicable test protocol with TSP for the selected grade.
A particle beta rating alone does not establish removal of deformable gels in a hot polymer melt.
Working Pressure and Differential Pressure
Working pressure concerns the pressurised process. Differential pressure is the pressure difference across the filter.
The published maxima are separate limits; they do not establish a combined operating envelope or a change out set point.
Specify normal and peak pressures, temperature, viscosity at the relevant shear conditions, start up transients and the approved terminal differential pressure.
Dimension Guide
Understanding D, d and H
Use these three dimensions to identify the basic disc envelope and centre opening. The plan view shows the disc face; the section shows the centre bore and axial height.
Leaf Disc Dimensions Explained
Outside Diameter | Centre Bore | Catalogue Height
Plan View
D is the outside diameter; d is the centre bore diameter. View along the disc axis.
Diametric Section
H is the catalogue height between the reference planes on the approved drawing. Axial thickness is enlarged for clarity.
D | Outside Diameter
The overall diameter measured across the outer edge of the disc.
Confirm the required clearance to the filter housing.
d | Centre Bore Diameter
The diameter of the central opening.
Confirm fit and tolerances with the mating collector or shaft.
H | Catalogue Height
The axial distance between the reference planes specified for that design.
Confirm whether the drawing measures across the hub, seal faces or another defined feature.
Drawing Check Before Ordering
State all dimensions in millimetres and confirm the current component drawing. H should not be assumed to equal the filter medium thickness or the assembled stack pitch.
Configurations and Dimensions
Selected Catalogue References
Group numbers identify the listed configurations; they do not classify the hub design.
Confirm current drawings, tolerances and the effective area of the supplied component.
Media, Hubs and Stack Sizing
Select the Complete Filtration Assembly
Available Constructions
Media and Hub Options
Media: sintered stainless steel fibre, multilayer sintered stainless steel wire mesh, or sintered metal powder.
Hub options: welded centre ring (hard hub) and centre ring (soft hub).
Sintered Fibre
A porous bonded fibre structure can provide depth capture.
Assess the balance of contaminant capacity, retention and clean resistance for the polymer.
Sintered Mesh
Woven layers offer a defined filtration structure with supporting layers.
Review the weave and full laminate, especially where hard particle contamination dominates.
Sintered Powder
A porous matrix of bonded particles provides another route for gel sensitive duties.
Compare tested performance and resistance; media names alone do not establish equivalence.
Filter Area and Surface Loading
Use the confirmed active area per disc when sizing a stack. A simple accounting example illustrates the calculation; it is not a throughput recommendation.
Count each disc’s confirmed total area once. Include any excluded end faces, seals or inactive zones in the supplier’s area definition. Stack count alone does not determine hydraulic capacity.
Verify the Hydraulics
Request pressure loss data for the actual polymer, temperature, throughput and complete stack. The review should include the media, internal drainage, inter disc spaces, collector and housing.
Application, Cleaning and Service
Build the Specification Around Film Quality
Film Quality and Performance
Leaf disc selection should address the film’s defect limits, polymer behaviour and operating economics.
Flow distribution, pressure loss and gel control should be assessed together.
Polymer and Production Duty
State resin family and grade, virgin/recycled blend, additives, melt temperature, viscosity basis, throughput range and the product being made.
Contamination and Quality Target
Describe hard particles, degraded polymer, gels and catalyst residues.
Supply retained contaminant samples or microscopy where available, and define the accepted film defect measure.
Existing Assembly
Provide the OEM or housing reference, disc drawing and revision, current medium and grade, hub type, seal details, disc count, spacers, stack height and change out history.
Trial and Performance Review
Compare candidate assemblies at matched melt conditions. Record initial differential pressure, its rise with time or tonnes processed, run length, film defects, breaks and off spec output. Include pressure transients and the reason for each change out in the trial record.
Cleaning and Return to Service
Use a cleaning sequence qualified for the polymer deposits, media, hub and weld construction. Following cleaning, evaluate flow resistance and integrity against an approved baseline and acceptance criteria for that filter design.
Visual cleanliness alone does not demonstrate restored filtration performance. Keep an individual record of service cycles, cleaning history, inspection results and test disposition; retire damaged discs or those outside the agreed criteria.
Polymer Filtration
Filter media selected for melt conditions and the required particle retention.
Material Selection
Match media construction to temperature, pressure and polymer compatibility.
Technical Support
Discuss filtration area, throughput and pressure drop for the application.